


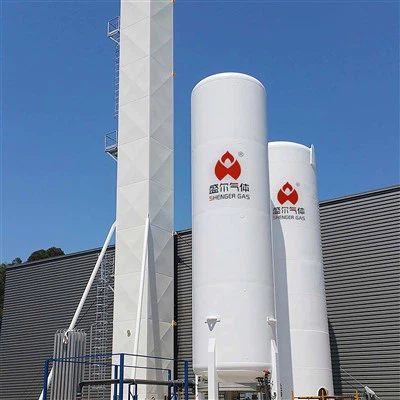
Large-Scale Air Separation Plant
Large-scale air separation plant engineering centers on a fundamental physical principle: the liquefaction and fractional distillation of atmospheric air. By compressing, purifying, and cooling air to cryogenic temperatures, this plant exploits the varying boiling points of oxygen, nitrogen, and argon to separate them with exceptionally high purity. The core mechanism-known as cryogenic rectification-operates within a tightly integrated cold box, where a dual-column system (high-pressure and low-pressure columns) enables continuous, high-purity product extraction.
Performance at a glance
| Parameter | Range / Value |
|---|---|
| Oxygen purity | 95% – 99.8% (typical) |
| Nitrogen purity | 99.999% (max) |
| Argon purity | 99.999% (max) |
| Flow capacity (O₂) | 1,000 – 80,000 Nm³/h |
| Operating temperature | -196°C – -183°C (main cold box) |
| Specific power consumption | 0.38 – 0.65 kWh/Nm³ O₂ (depending on pressure) |
These figures demonstrate the plant's ability to adapt to both tonnage oxygen and high-purity nitrogen demands.
Why this matters for industrial gas producers
A well-engineered large-scale air separation plant delivers more than just product-it delivers operational stability. The temperature window is maintained through a balanced turbo-expander and heat exchanger network, ensuring minimal cold loss. Energy consumption, often the single largest operating cost, is contained via advanced radial-flow adsorbers and structured packing internals, which reduce pressure drop and improve mass transfer. Typical specific power for oxygen production ranges from 0.38 to 0.65 kWh/Nm³, while nitrogen generation can fall below 0.18 kWh/Nm³ under optimised conditions.
Technical specifications
These are not static; they shift with site conditions (ambient temperature, cooling water availability, and elevation). However, a standard skid-mounted configuration might include:
- Main air compressor: centrifugal, 3–15 bar(g)
- Purification unit: molecular sieve adsorbers (dual-bed, TSA cycle)
- Cold box: packed column / sieve tray, stainless steel construction
- Expander: oil-free turbo-expander with magnetic bearings (optional)
- Product pressures: O₂ at 1.5–30 bar(g); N₂ at 1.5–80 bar(g)
Industrial applications
Beyond steelmaking and chemical synthesis, these plants are essential for:
- Electronic-grade nitrogen for semiconductor fabrication
- Oxygen enrichment in glass melting and non-ferrous smelting
- Syngas adjustment in methanol/ammonia production
- Liquid backup systems for peak-shaving and emergency supply
Certifications and compliance
Every large-scale air separation plant is designed to meet ASME, PED, GB/T, and ISO 9001/14001 standards. Pressure vessels are certified per local statutory requirements, and all rotating equipment follows API 617/672 where applicable. Hazardous area electricals comply with ATEX or IECEx as specified.
Customisation capability
- Modular vs. field-erected structures
- Driver selection (steam turbine, motor, or engine)
- Argon recovery systems (crude or pure)
- Remote I/O and DCS integration (Siemens, Yokogawa, Honeywell)
- Cold box layout tailored to seismic zones and space constraints
Service beyond delivery
Commissioning support, operator training, and predictive maintenance plans are included. Our after-sales team provides vibration analysis, chromatograph calibration, and performance guarantee tests within 12 months of start‑up. Spare parts are stocked regionally to minimise downtime.
For a large-scale air separation plant to truly perform, it must be engineered not just for today's feed conditions but for tomorrow's process flexibility. That is why Shenger Gas integrates every unit-from air intake to product storage-into a coherent system with transparent control logic and fail‑safe interlocks. We do not simply supply equipment; we supply the thermodynamic certainty that your production line relies on every shift. Choose Shenger Gas for a partner that speaks the language of cryogenic engineering and delivers plant performance you can measure-not just promise.


Hot Tags: large-scale air separation plant, China large-scale air separation plant manufacturers, suppliers, factory, Cryogenic Liquid Nitrogen Plant
You Might Also Like




Send Inquiry