


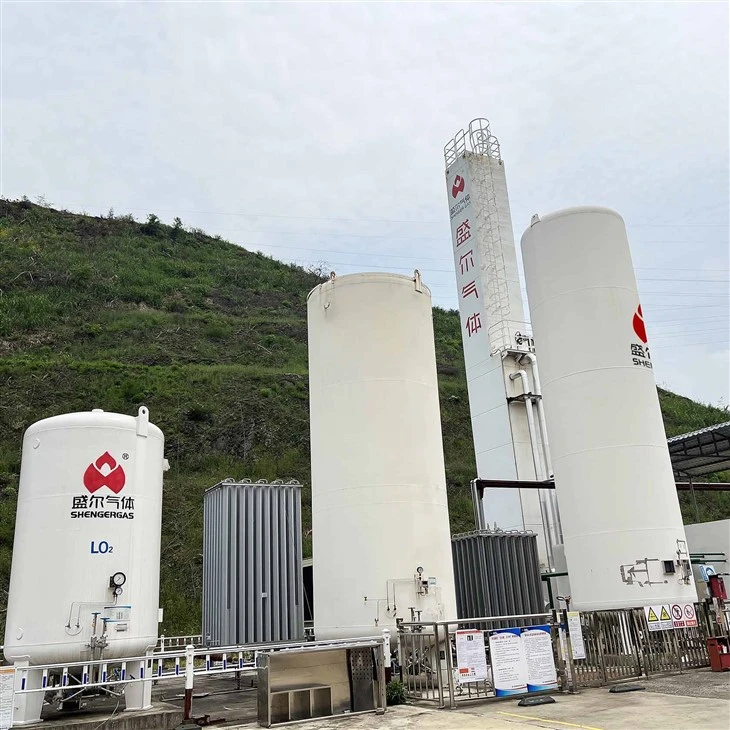

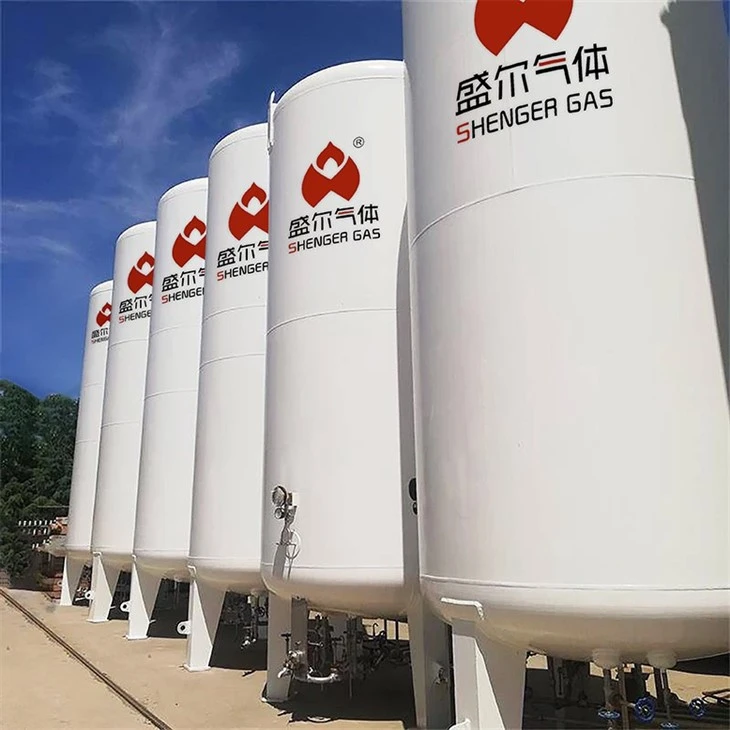
ASU Plant
Cryogenic air separation technology is the most mature and economical method for large-scale oxygen, nitrogen and argon in the field of modern industrial gas separation. As a large industrial gas device, ASU Plant compresses, cools, liquefys the air, and uses the differences in boiling points of each component in the air to distillate and separate them in the distillation tower, and finally obtains high-purity oxygen, nitrogen and argon.
Unlike pressure-switch adsorption and membrane separation technologies, ASU Plant is particularly suitable for large-scale, high-purity industrial gas production needs, and the oxygen production capacity of a single set of devices can reach tens of thousands of cubic meters per hour. This technology is mature and reliable, and has stable operation, and is an indispensable key equipment in the fields of modern steel smelting, chemical synthesis, coal chemical and other fields.
Core advantages of the product
Our ASU Plant uses state-of-the-art cryogenic air separation technology to provide customers with efficient and reliable large-scale gas solutions:
- Large-scale production capacity: the oxygen production capacity of a single set of devices ranges from 1000Nm³/h to 100,000Nm³/h, meeting the gas needs of large industrial users
- High-purity products: can simultaneously produce more than 99.6% high-purity oxygen, 99.999% high-purity nitrogen and 99.999% high-purity argon
- Low-energy design: adopting high-efficiency compressor, molecular sieve purification system and boost expander to significantly reduce unit energy consumption
- Automated operation: fully automatic control system, realize unattended operation, remote monitoring of operation status
- Reliability and durability: The key equipment adopts internationally renowned brands to ensure long-term and stable operation of the device
Technical Parameters
|
Parameter Item |
Specification Range / Description |
|
Oxygen Purity |
95% ~ 99.8% (Adjustable, standard 99.6%) |
|
Nitrogen Purity |
99.999% (Atmospheric pressure dew point ≤ -70°C) |
|
Argon Purity |
99.999% (Argon production system optional) |
|
Oxygen Production Capacity |
1,000 ~ 100,000 Nm³/h (Customizable according to requirements) |
|
Nitrogen Production Capacity |
1,000 ~ 200,000 Nm³/h (Customizable according to requirements) |
|
Operating Temperature |
Distillation column operating temperature: -175°C ~ -195°C |
|
Operating Pressure |
Lower column: 0.5-0.6 MPa, Upper column: 0.04-0.05 MPa |
|
Energy Consumption Index |
0.38 ~ 0.52 kWh/Nm³O₂ (Varies depending on scale and configuration) |
|
Start-up Time |
24-48 hours (From ambient temperature to normal operating conditions) |
|
Continuous Operation Time |
≥ 2 years (Overhaul cycle) |
Industry applications
Our ASU Plant is widely used in the following industries:
- Iron and Steel Metallurgy: Blast furnace oxygen-rich blower, converter steelmaking, continuous casting and cutting, and nitrogen protection of rolling steel
- Chemical industry: coal chemical industry, fertilizer production, ethylene cracking, oxidation reaction oxygen supply
- Nonferrous metals: metal smelting processes such as copper smelting, aluminum processing, zinc smelting, etc.
- Glass manufacturing: float glass production line, glass melting kiln oxygen to ignite
- Papermaking industry: Oxygen use in bleaching process, pulp oxidation treatment
- Sewage treatment: activated sludge oxygen aeration, industrial wastewater treatment
- Petrochemical: Refinery catalyst regeneration, petrochemical product refining
System composition
A complete set of ASU Plants usually includes the following main systems:
- Air compression system: main air compressor, air pre-cooling system
- Air purification system: molecular sieve adsorber, CO₂ and moisture removal
- Heat exchange system: main heat exchanger, condensation evaporator, supercooler
- Distillation system: lower tower, upper tower, crude argon tower, refined argon tower
- Product compression system: oxygen compressor, nitrogen compressor
- Control system: DCS distribution control system, ESD emergency parking system
Certification standards
We design and manufacture cryogenic air separation equipment strictly in accordance with international standards:
- ISO 9001:2015: Quality Management System Certification
- ASME BPVC Section VIII: Pressure Vessel Design and Manufacturing Specifications
- PED 2014/68/EU: EU Pressure Equipment Directive
- GB150: China Pressure Vessel Standard
- CE certification: Products comply with European safety standards
- API standards: compressors, pumps and other rotating equipment comply with API standards
Frequently Asked Questions
Q: How long does the construction cycle of cryogenic air separation equipment take?
A: Depending on the scale of the device, it usually takes 12-24 months from contract signing to production, including design, procurement, manufacturing, installation and commissioning.
Q: What is the energy consumption level of the equipment?
A: The unit oxygen energy consumption of modern large-scale air separation equipment is usually between 0.38-0.52 kWh/Nm³, depending on the device size, product structure and configuration plan.
Q: How long is the overhaul cycle of the equipment?
A: It is usually recommended to conduct planned parking maintenance every 2-3 years, mainly to inspect key equipment such as molecular sieve, heat exchanger and compressor.
Q: Can gas storage and backup systems be provided?
A: We can provide complete solutions, including liquid oxygen, liquid nitrogen storage tanks and gasification systems, ensuring the safety of users' gas supply.
Our Services
Shenger Gas provides customers with comprehensive service support:
- Project feasibility study and program design
- Equipment manufacturing, installation and commissioning
- Operator training and technical guidance
- Supply and inventory management of spare parts
- Equipment performance optimization and transformation and upgrading
- 24-hour emergency technical support service
Contact our technical team now to get customized cryogenic air separation solutions! Let us provide you with the most suitable ASU Plant to meet your large industrial gas needs!


Hot Tags: ASU Plant, China ASU Plant manufacturers, suppliers, factory, Cryogenic Liquid Nitrogen Plant, , , ,
You Might Also Like


Send Inquiry