


Cryogenic ASU for Petrochemical Industry
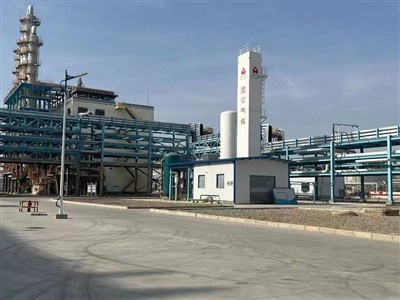
Cryogenic ASU for petrochemical industry uses advanced cryogenic distillation technology, designed for the petrochemical industry to efficiently produce high-purity oxygen, nitrogen and argon. Through the low-temperature air separation process, the system provides stable and reliable gas supply for petrochemical production, meeting the key process needs of oil refining, ethylene cracking, coal chemical industry, etc. Cryogenic ASU for petrochemical industry has the characteristics of high energy efficiency, long-term operation and intelligent control, and is an indispensable core equipment for modern chemical production.
Core Specifications & Technical Parameters
|
Item |
Parameter / Description |
|
Product Series |
Large-scale cryogenic ASU (1000~100,000 Nm³/h) |
|
Oxygen Purity |
99.6%~99.9% (higher purity available upon request) |
|
Nitrogen Purity |
99.999% (PPB grade optional) |
|
Argon Purity |
≥99.999% (for fine chemical applications) |
|
Operating Temperature |
-196°C (distillation column operating temperature) |
|
Energy Consumption |
0.35~0.55 kWh/Nm³ O₂ (industry-leading level) |
|
Operating Pressure |
0.5~6.0 MPa (configurable per process requirements) |
|
Industry Applications |
Refinery hydrocracking, ethylene plants, ammonia synthesis, coal-to-liquids/gas, PX projects |
|
Key Technologies |
High-efficiency molecular sieve purification, expander energy recovery, fully automated DCS control |
|
Compliance Standards |
ISO 7396 (medical gas standards), ASME BPVC (pressure vessel code), GB/T 16912 |
|
Control System |
ESD emergency shutdown + redundant DCS control, supports remote diagnostics |
|
Optional Configurations |
Liquid oxygen/nitrogen backup system, argon recovery unit, VOCs treatment module |
Industry application scenarios
- Oil refining process: Provide 99.6% high-purity oxygen for hydrocracking and catalytic reforming to improve oil quality
- Ethylene production: Oxygen-rich combustion of cracking furnaces, reducing energy consumption by 15%~20%
- Coal Chemical Industry: Oxygen used for coal gasification, pressure matching to 6.0MPa
- Environmental protection field: supporting sulfur recovery device (Claus process)
Technical Advantages
- Energy-saving design: adopts three-stage expander + thermal coupling technology, and the energy consumption is reduced by 12% compared with traditional equipment.
- Long cycle operation: the life of key equipment is ≥15 years, the continuous operation cycle is >3 years
- Intelligent control: AI predictive maintenance system, real-time optimization of distillation tower working conditions
Certification and Service
- International certification: ASME U steel stamp, PED 2014/68/EU, SIL3 safety level
- Project experience: Cumulatively provide 70+ large-scale installations for the Middle East/Asia-Pacific region
- Service guarantee: 24-month warranty period, lifelong technical support
As a professional manufacturer of air separation equipment, Shenger Gas is committed to providing high-performance cryogenic ASU for petrochemical industry solutions to the petrochemical industry. With years of industry experience and technical accumulation, we provide global customers with full-process services from design, manufacturing to installation and commissioning, ensuring the stable operation of equipment in key processes such as oil refining, ethylene, coal chemical industry, etc.
About us
Shenger's capital investment in talents and scientific research accounts for more than 7% of whole sales, and always insists on creating its own golden business card of high efficiency, innovation and energy saving. Maintain long-term and stable cooperation with world-class well-known enterprises, such as Germany's Siemens, BURKERT, GEMU, and Japan's Takeda Corporation, Iwatani Corporation, etc.

Our Product
Shenger's products are divided into the following categories: various gas purification devices, PSA nitrogen plant, PSA oxygen plant, VPSA oxygen plant, waste heat regeneration air dryers, heatless regeneration dryers, micro-heat regeneration dryers, refrigerated type Dryers, combined dryers, cryogenic air separation plants, etc.
OEM/ODM
When you put forward your needsour engineers will provide you withfaster and more perfect customizedsolutions. We have a wide range ofproducts, and we will provide technical support according to youractual needs to choose the rightproduct for you.
Production Equipment
Forklift, Single beam crane, Sawing machine, Radial drilling machine, SCR DC arc welding machine, Gas shielded welding machine, Paint room, PPCW chuck pipe welding center, Shot blasting machine, Vibrating platform
Factory Strength
The factory building and office area are about 10,000 square meters, with various imported production equipment. Shenger Gas has a complete production process, which can meet customers' needs for customized molecular sieve nitrogen generators and oxygen generators.
Our Certifications


FAQs
Q: What is your factory product range?
Q: How long does the normal delivery time take?
Q: What is the term of payment?
Q: Do you offer oDM services?
Q: Where is your factory,can we visit it?
Welcome to visit the factory at anytime.
Hot Tags: Cryogenic ASU for Petrochemical Industry, China Cryogenic ASU for Petrochemical Industry manufacturers, suppliers, factory, Cryogenic Liquid Nitrogen Plant, , , ,
You Might Also Like


Send Inquiry